Beverage filling machine manufacturer Complete filling line solution set

King Machine is a well-known manufacturer of filling machines with over 20 years of export experience. It can provide complete turnkey filling line solutions for water, juice, carbonated beverages, edible oil and daily chemical products.
You are here:Home » Knowledge Graph

Blow molding machine knowledge graph

The key components, manufacturing processes, typical faults, maintenance items and safety rules of the machine.
Preform heating head module
Component Part Preform Heating Head Module
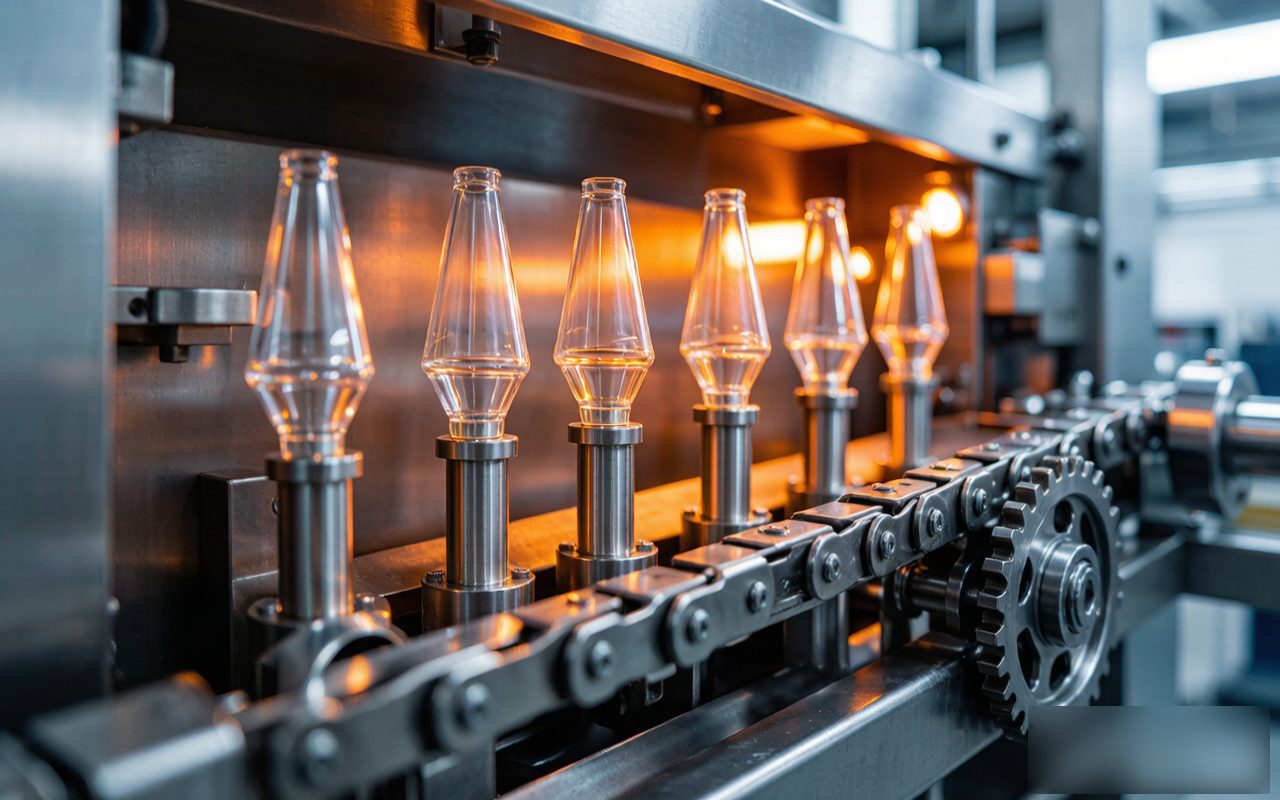
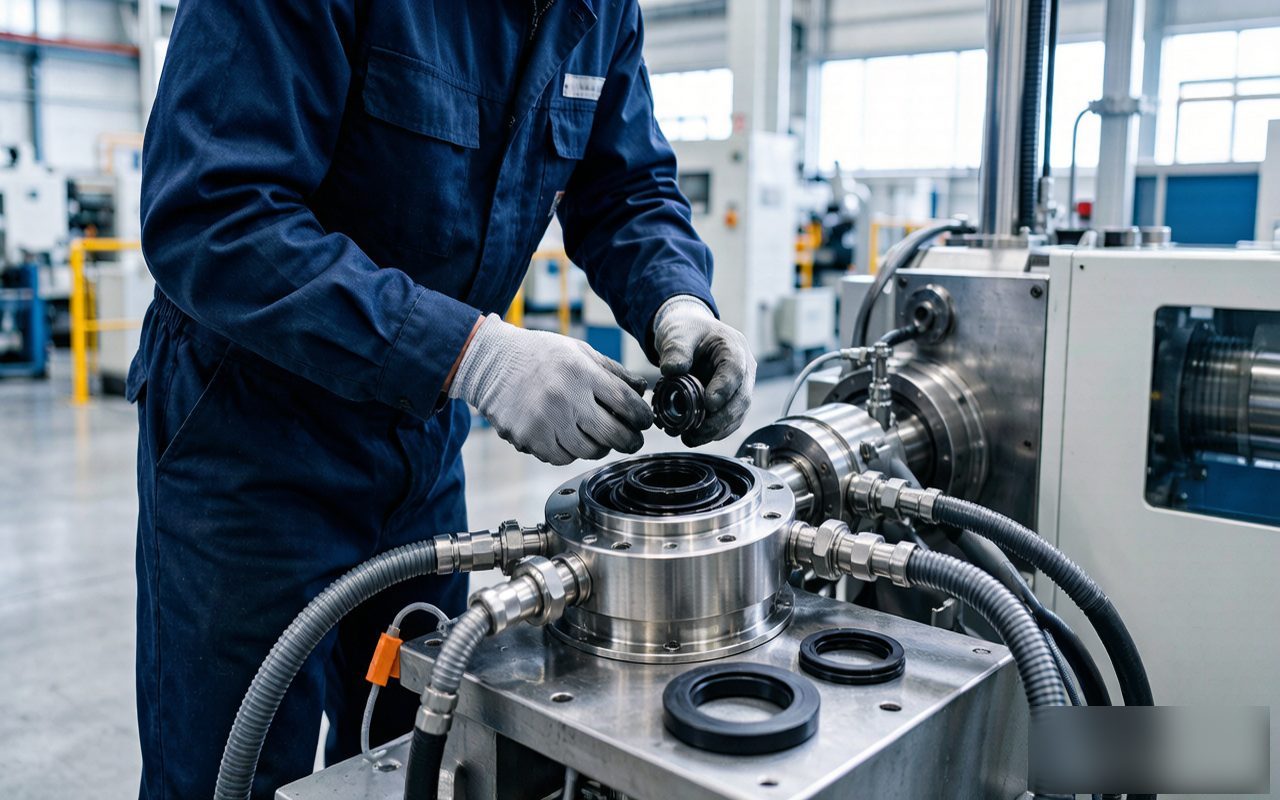
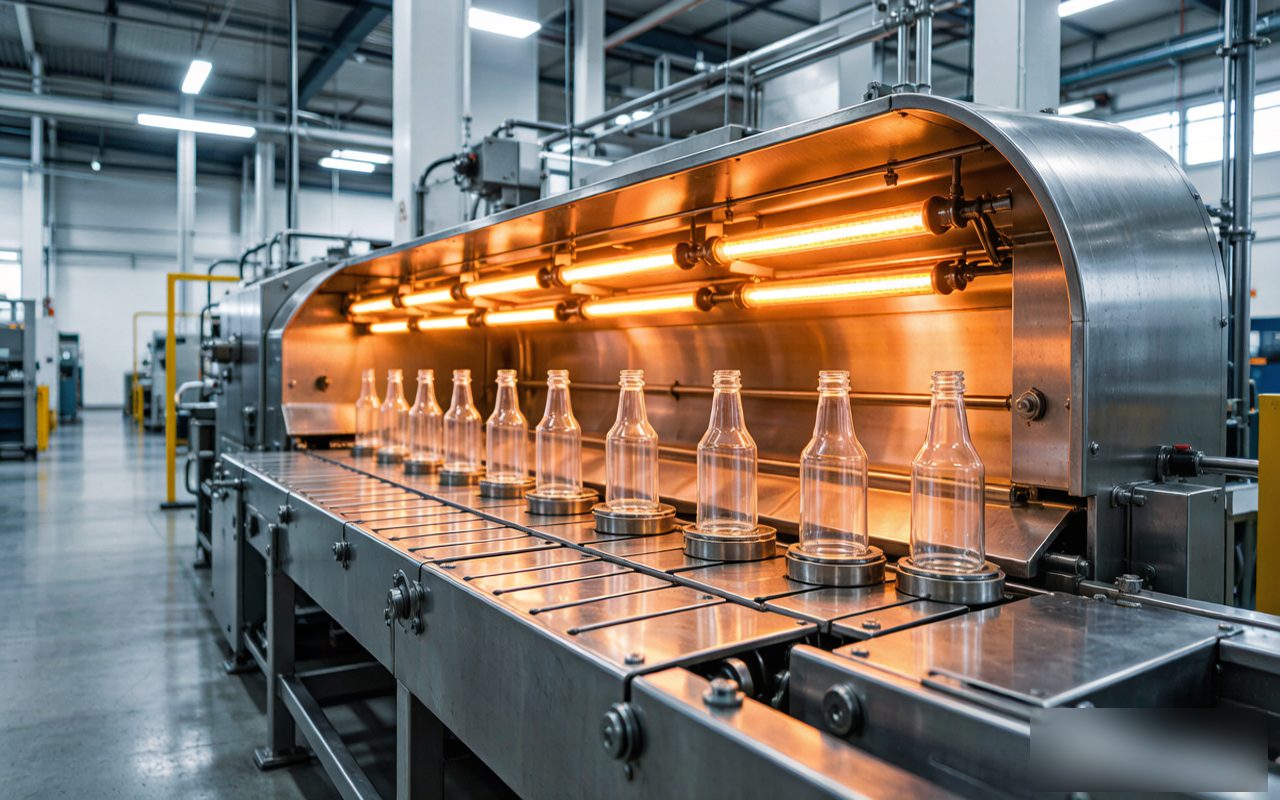
Each preform is carried by one heating head. The chain fixed on the heater frame meshes the upper and lower sprockets and drives the expansion sleeve, chuck and unloading ring, so the preform rotates through the light boxes and is heated evenly before blowing.
Part No.9 & S3 · every 5,000 h Part No.13 · every 7,500 h
Stretch blow molding process
Process Stretch Blow Molding Process
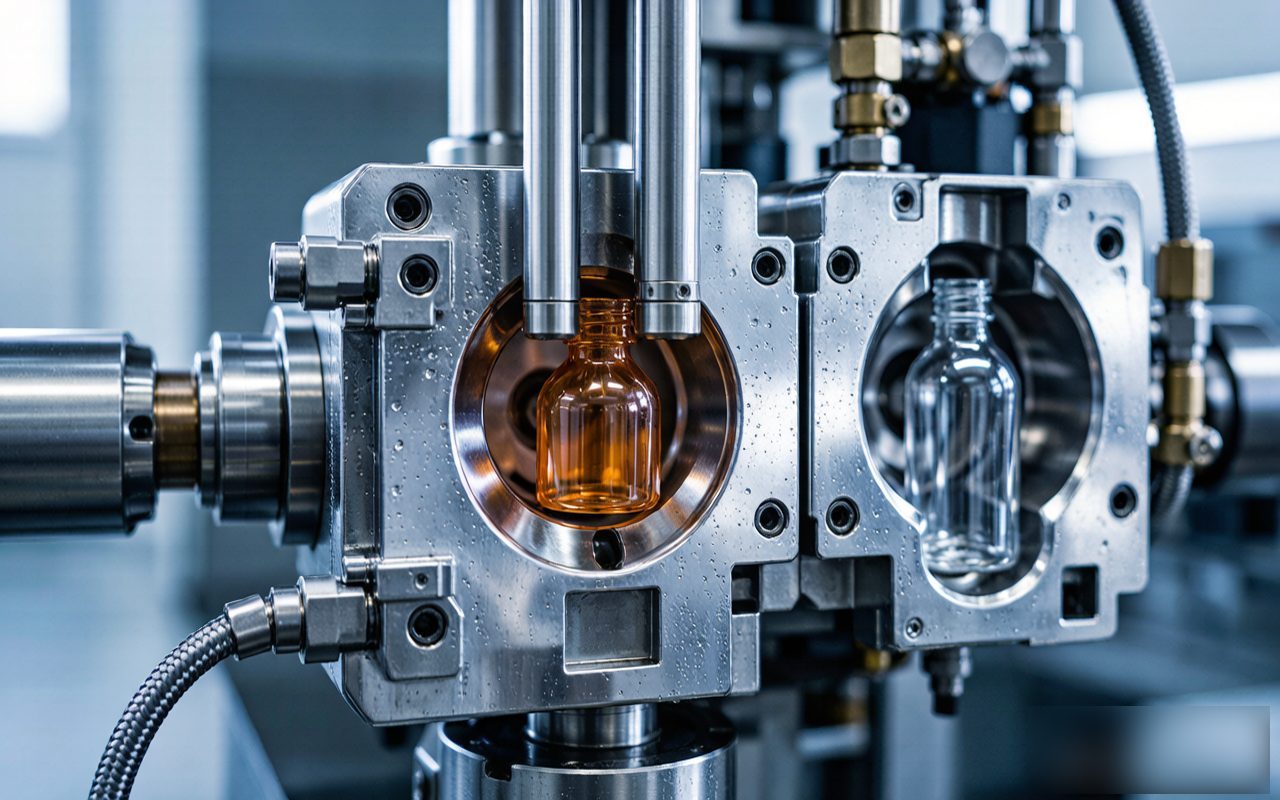
After the heated preform is locked in the mould, the stretch rod stretches it axially while the sealing cylinder seals the neck and blows. Pre-blow at 6–13 bar pre-shapes the bottle, then the second blow at 40 bar forms it against the mould wall.
Pre-blow 6–13 bar Final blow 40 bar
Heater cannot load preform
Fault Heater Cannot Load Preform
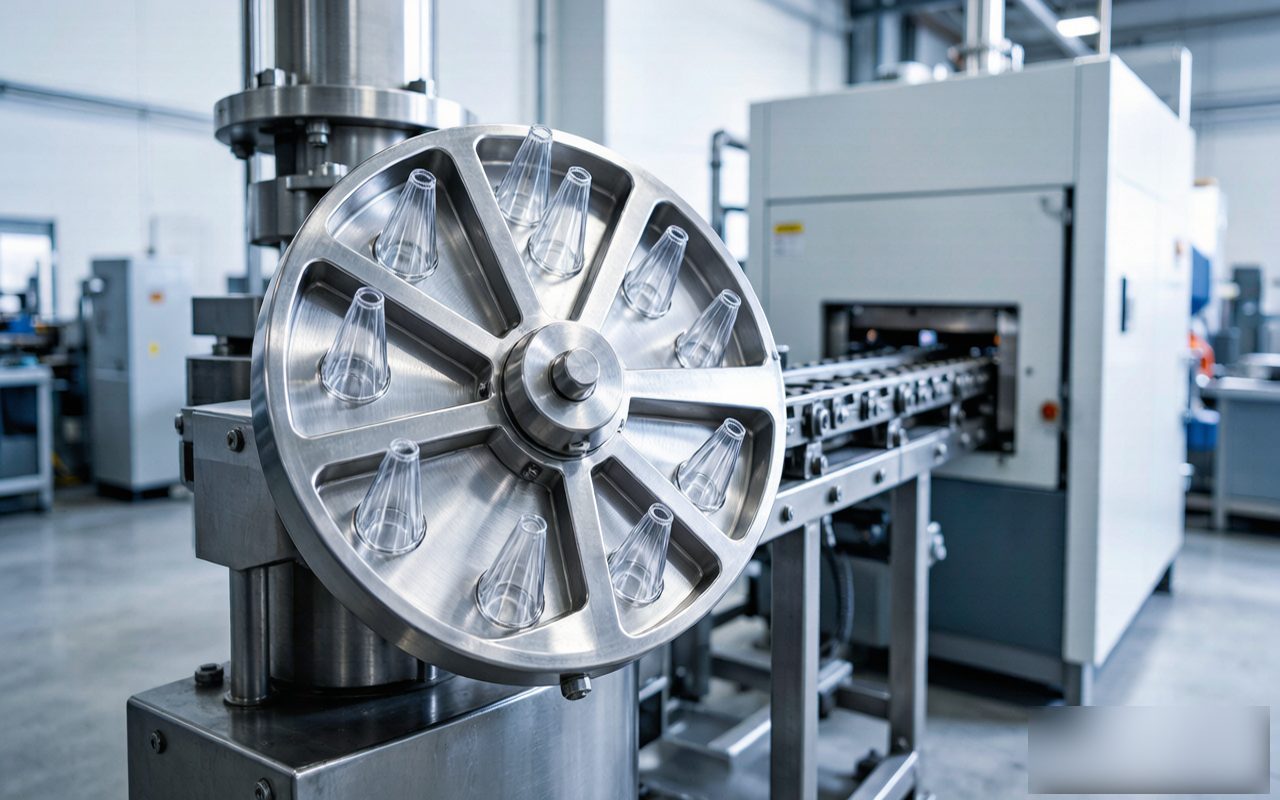
The preform track of the infeed starwheel is not tangent to, and not synchronised with, the preform track of the heater chain; or the loading position of the load / unload device is wrong. Adjust the relative position of starwheel and chain until loading is centred.
Adjust starwheel / chain position Synchronise loading position
Heating head wear parts replacement
Maintenance Job Heating Head Wear Parts Replacement
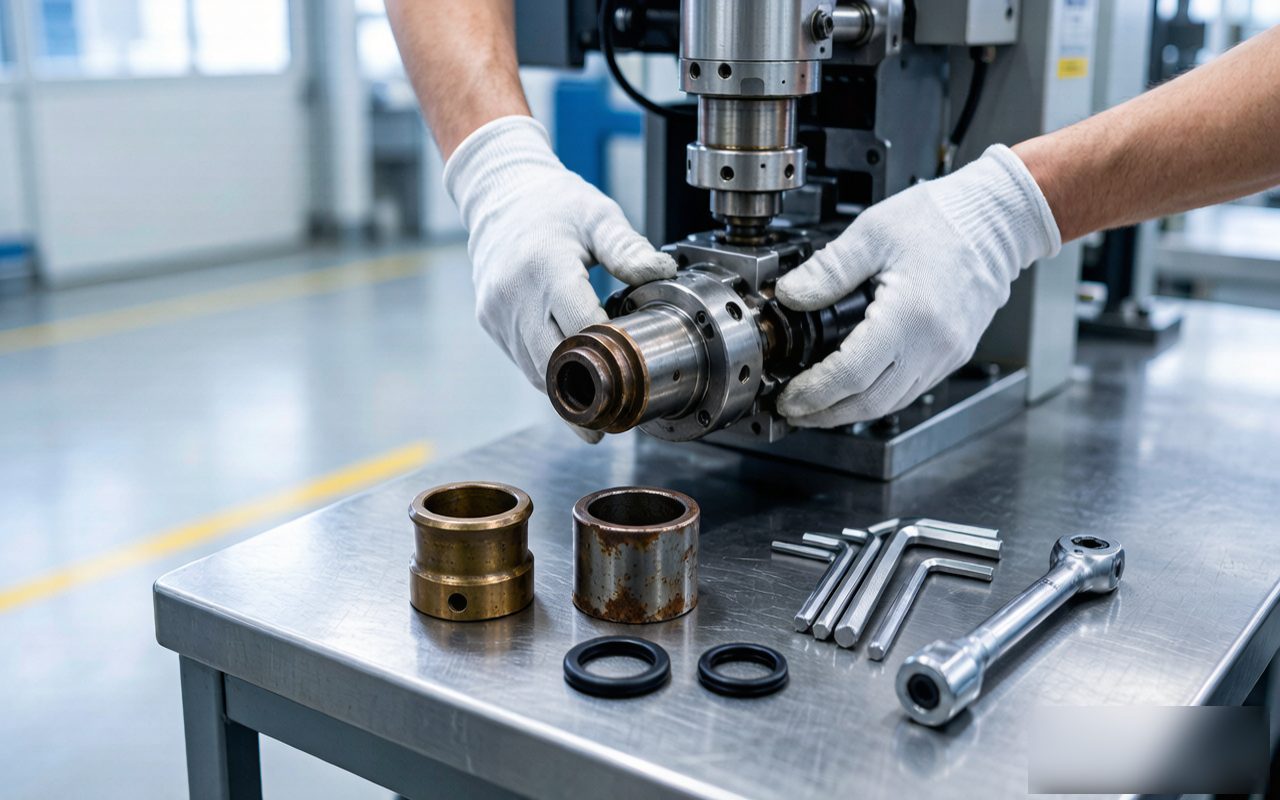
Renew the bush and the O-ring (No.9 / S3) after 5,000 running hours, and part No.13 after 7,500 hours. Replace them as a complete set so that every preform keeps rotating truly and is heated uniformly.
Cycle 5,000 h Cycle 7,500 h
Water distributor repair kit replacement
Maintenance Job Water Distributor Repair Kit Replacement
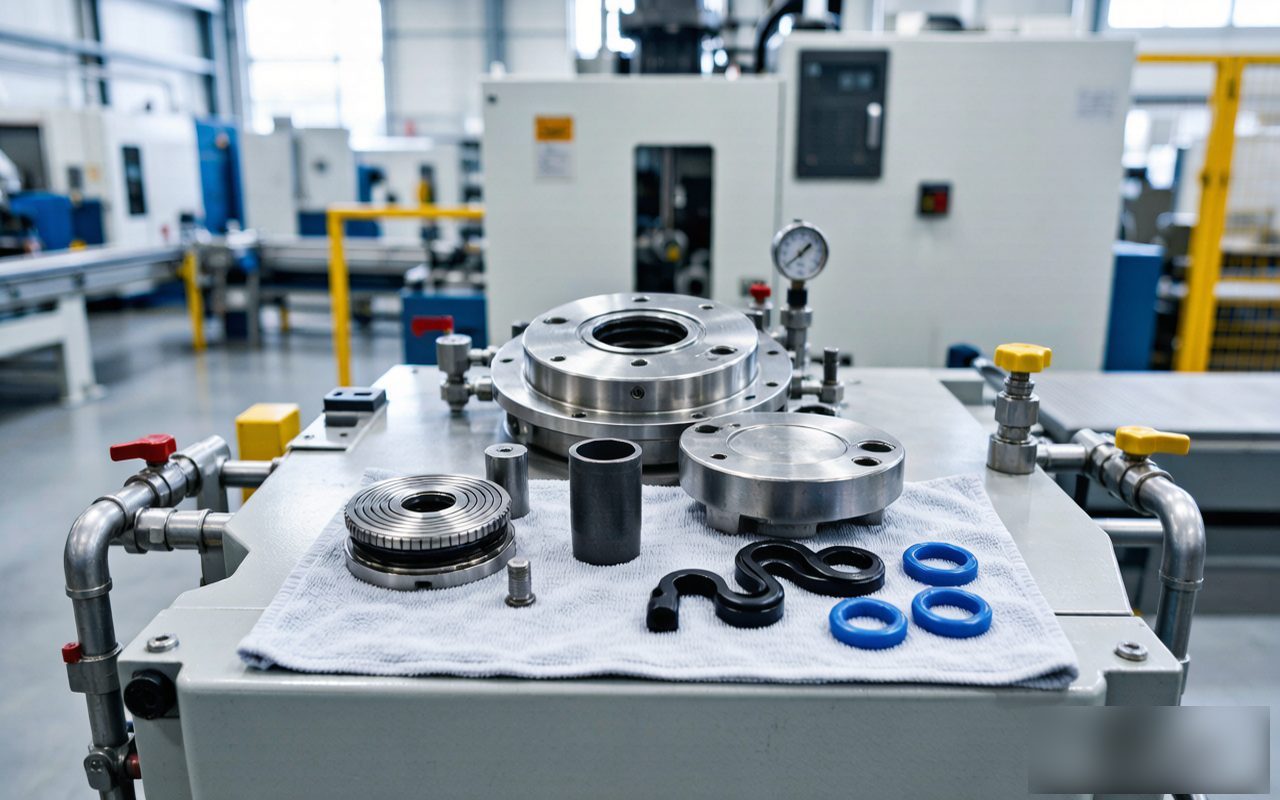
When leakage appears at the connections, take the water distributor off and renew the mechanical seals one by one — the seal set in the inlet kit, the seals inside the rotary sleeve and the remaining seals on the tubes.
Trigger: water leakage Mechanical seal type
Air distributor seal replacement
Maintenance Job Air Distributor Seal Replacement
Switch off power, air and water and brake the machine before starting. Then remove the conductive slip ring, stopper, press cover and connecting seat to renew the S-type roto glyd rings and O-rings; refit in the reverse order and clean the site.
Power / air / water off Refit in reverse order
Lockout before any maintenance job
Safety Rule Lockout Before Any Maintenance Job
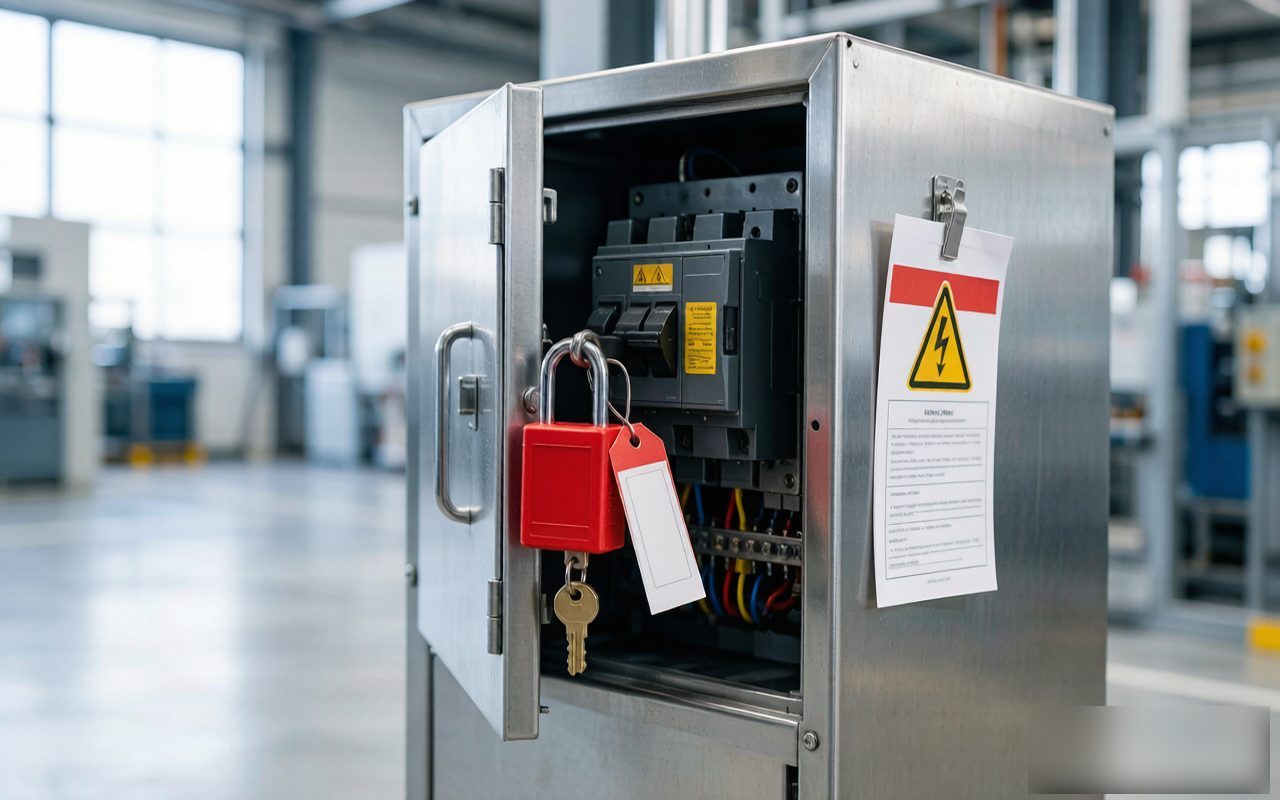
Once the machine is stopped it must be locked to prevent it from being switched on again. Every person working on the machine uses his own lock and carries the key; no lock may be removed before the job is finished. Hang a maintenance warning sign.
Own lock & key Warning sign board

Browse Equipment Knowledge Base by Category

Built around the blow molding machine (XC8-00), this section gathers knowledge nodes for components, processes, faults and maintenance. Switch categories above to view the corresponding content; more equipment types will be added over time.
Blow Molding Machine
Filling Machine
Capping Machine
Conveying System
  • Preform heating head module
    Preform Heating Head
    Composed of the expansion sleeve, sprocket and self-rotating spindle, the preform spins evenly along the chain through the infrared heating lamps to ensure uniform circumferential heating; wear parts are recommended to be replaced every 5000 h / 7500 h.
  • Stretch blow molding process
    Stretch Blow Molding
    Pre-blow at 6–13 bar pre-expands the preform, the stretch rod descends for positioning, and the second blow at 40 bar forms it against the mould cavity; temperature and air pressure together determine wall thickness and clarity.
  • Common faults and troubleshooting
    Faults & Troubleshooting
    Typical faults include the heater failing to load preforms, starwheel misalignment jamming the preform, and uneven heating causing a milky bottle body; corresponding checks cover the infeed starwheel phase, lamp status and chain tension.
  • Maintenance and safety
    Maintenance & Safety
    Before maintenance the machine must be stopped and locked out (LOTO); regularly replace heating-head wear parts and water/air distributor seals, and inspect lubrication and filter cartridges to keep the equipment stable and personnel safe.

Video Guides

Short clips of the preform heating tunnel, the stretch blow forming station and routine maintenance. Swipe the carousel or click the dots to switch between videos.

XC8-00 Machine Overview

A full walkthrough of the blow molding machine: preform infeed, the infrared heating tunnel, the stretch blow forming station and the discharge starwheel.

Preform Heating & Temperature Control

Preforms rotate on self-driven spindles while passing the infrared lamps, so the wall is heated evenly; lamp power and chain speed set the final temperature profile.

Stretch Blow Molding Cycle

Pre-blow at 6–13 bar pre-expands the preform, the stretch rod descends for positioning, and the second blow at 40 bar forms the bottle against the mould cavity.

Maintenance & Lockout Safety

Always stop and lock out the machine (LOTO) before service; replace heating-head wear parts and water / air distributor seals on schedule, and check lubrication points.
Free Consultation

Tell Us About Your Bottling Project

Send your bottle size, target output and filling type — our engineers will reply within one working day with a suitable machine configuration and a quotation.
Get a Free Quote→
×

Contact Us